Large Cold Room
- Superior Quality
- User-Friendly Design
- Food Safety Compliance
- Ensures Long-term Performance
- Exceptional Load-Bearing Capacity
Your Premier Large Cold Room Manufacturer in China
Sunnyda’s large cold rooms are meticulously crafted using a high level of attention to detail. These cold rooms feature insulated panels that are constructed using two steel sheets encasing a core made of high-density polyurethane. These panels are precisely engineered to form the walls, ceiling, and floor of the cold room, which ensures exceptional insulation and structural integrity.
The refrigeration system, which incorporates a reliable Bitzer compressor, is carefully designed to maintain the precise temperature required for optimal storage conditions. This system ensures that the environment maintains the perfect temperature for the stored products.
Additionally, Sunnyda’s control system, housed within a thoughtfully designed control panel, orchestrates the seamless operation of the entire system. This ensures that every component works together efficiently and effectively.
Sunnyda’s large cold room is equipped with a sturdy and airtight door, available in sliding or hinged options to securely seal the environment to provide you with easy access and high security.
- Data Sheet
| Type | Application | Typical Size (m³) |
| Chiller Rooms | Fresh produce, dairy, meat, beverages | 30-250 |
| Freezer Rooms | Frozen food, ice cream, processed food | 20-260 |
| Blast Freezing Rooms | Rapid freezing of food | Varies based on production |
| Ultra-Low Temperature (ULT) Freezers | Biological samples, vaccines, pharmaceuticals | 10-55 |
| Walk-in Cold Rooms | Various products, supermarkets, restaurants | 25-550 |
| Reach-in Cold Rooms | Limited storage, kitchens, retail stores | 10-25 |
| Bulk Cold Stores | Large quantities of a single product | 400+ |
| Multi-temp Cold Stores | Products with different temperature requirements | Varies based on product mix |
| Mobile Cold Storage | Transporting perishable goods | Varies based on vehicle size |
| Modular Cold Rooms | Flexible installation, various needs | Customizable |
| Custom-Built Cold Rooms | Unique needs, tailored solutions | Customizable |
| Cold Storage Warehouses | Bulk storage and distribution | 900+ |
| Large Cold Storage Facilities | Mass storage, distribution centers, logistics | 4000+ |


Advantages of Sunnyda Large Cold Room
Customizable
Sunnyda’s expertise lies in creating tailored cold storage solutions that are uniquely suited to the specific needs of your business. Whether you need a facility for storing pharmaceuticals, food items, or other temperature-sensitive products, Sunnyda can provide custom-designed options that precisely match your requirements.
Sunnyda’s adaptable approach enables us to address a variety of space limitations and deliver solutions that go above and beyond your expectations. Committed to versatility, we design personalized cold storage facilities that seamlessly align with your commercial needs.


Built to Last
Sunnyda’s cold storage systems are expertly designed to prioritize longevity and reliability. We meticulously construct them using high-quality materials and reinforce them with strong components to ensure that they can endure the demands of continuous operation.
At the core of Sunnyda’s systems lies an efficient and durable cooling technology that is engineered to provide you with consistent performance over prolonged periods. This steadfast dedication to quality guarantees an extended service life, reducing downtime and optimizing the return on your investment.
Fire Resistant
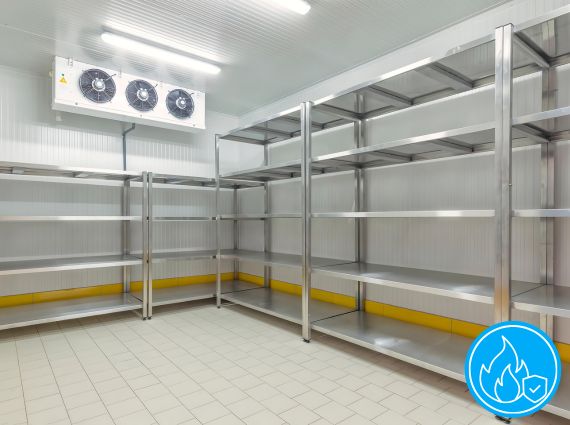
Sunnyda’s large cold rooms are meticulously designed with a strong focus on fire safety. These facilities are constructed using non-flammable materials to create a secure environment for your valuable products.
The walls, ceilings, and doors are all equipped with fire-resistant features to provide you with comprehensive protection against potential hazards.
With Sunnyda’s cold rooms, you can have peace of mind knowing that your products are stored in a facility that prioritizes safety and security.
Has a Large Cold Room Storage Capacity
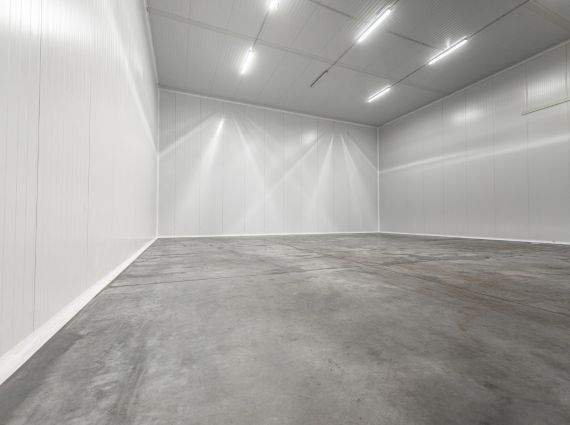
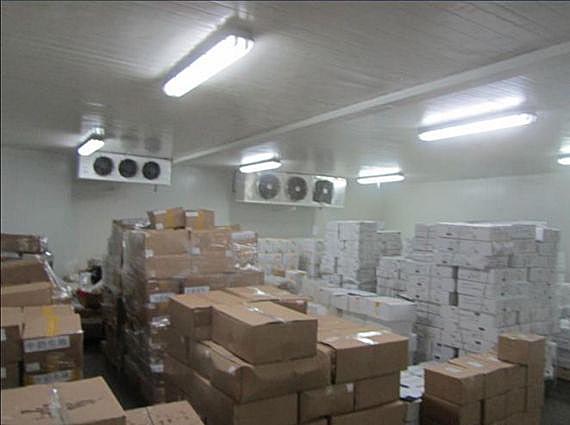
Sunnyda’s large cold rooms are meticulously designed to offer extensive storage capacity while effectively managing space and promoting efficient organization.
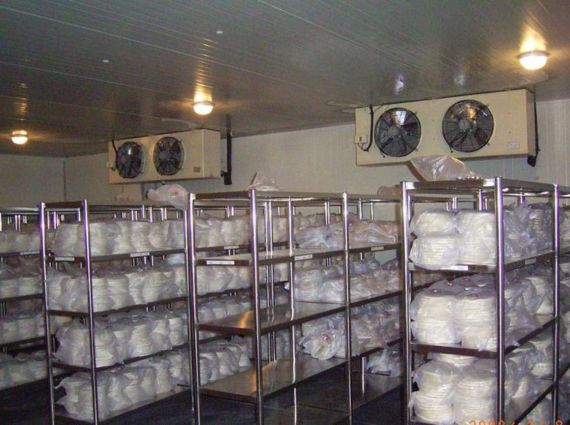
Our cutting-edge facilities are equipped with high-weight capacity flooring and high-density shelving, both of which contribute to maximizing storage space and providing you with secure protection for your valuable products.
By incorporating generous service spacing and prioritizing a compact design, Sunnyda guarantees that your storage area is utilized to its full potential, allowing you to make the most of every square inch.
Reduce the Risk of Contamination
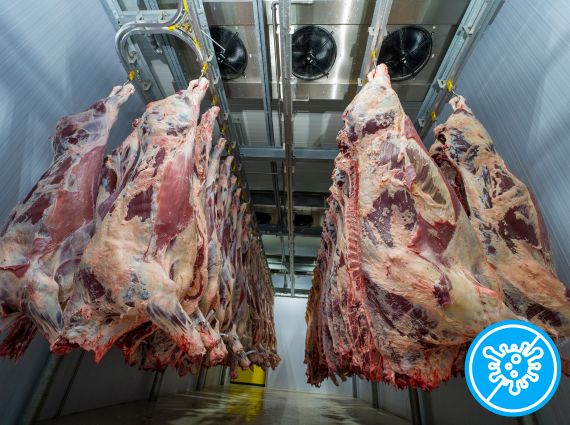
Sunnyda’s large cold rooms are carefully crafted to keep your food safe and fresh. The rooms are built with antimicrobial coatings and utilize hygienic food-grade stainless steel and aluminum interiors to ensure durability and ease of cleaning.
These features are designed to minimize the risk of bacterial, mold, and pathogen growth, helping you create a clean and safe work environment.
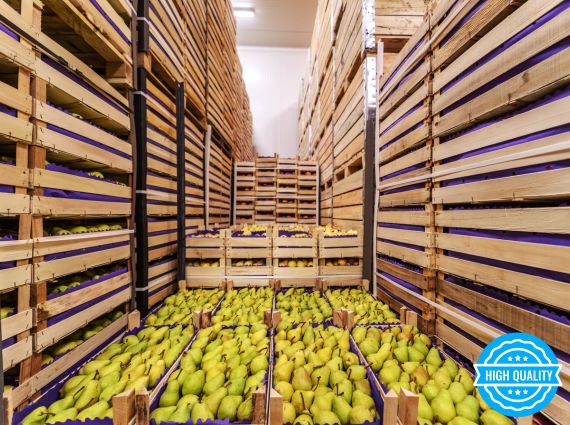
Preserve Product Quality
Sunnyda’s large cold rooms are specifically engineered to maintain precise low temperatures that are optimal for the safe storage of perishable goods.
These cold rooms effectively preserve the quality of perishable items, allowing for extended storage without compromising their essential properties.
In Sunnyda’s large cold room, you can confidently store and preserve a wide range of perishable products while maintaining their freshness and integrity.
Prioritize Safety
Sunnyda’s large cold rooms are meticulously designed to prioritize safety in every aspect. From the anti-slip flooring that minimizes the risk of accidents to the inclusion of emergency personnel alarms, we leave no stone unturned in providing you with a safe environment.
To facilitate safe loading and unloading, our cold rooms feature fixed ramps that provide a stable surface for the movement of goods. In the unfortunate event of an emergency, the cold rooms are equipped with an internal door release/escape hatch, offering a reliable means of exit. Our doors are intricately engineered to prevent back injuries and allow you smooth and effortless opening and closing.
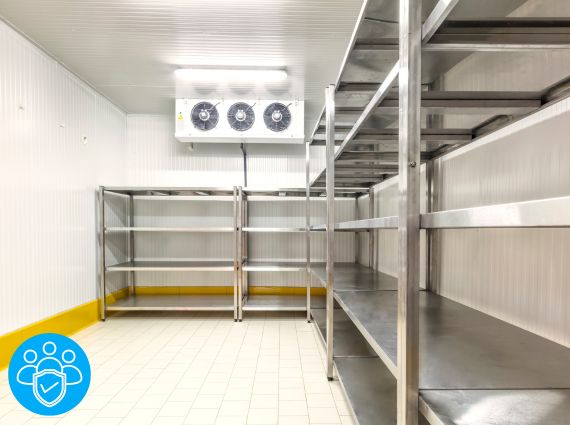

Built with High-Quality Materials
Sunnyda’s large cold rooms are built using high-quality materials and the latest refrigeration technology to ensure efficiency and reliability. They have a user-friendly touchscreen control interface and fully automatic control, making them simple to operate.
The insulated tongue and groove construction with cam-locking not only ensures precise temperature control but also promotes energy efficiency.
The cold rooms are equipped with custom lighting systems, insulated glass viewports, and advanced reliability features to provide you with a user-friendly and efficient cold storage solution.
Excellent Quality Control and After-Sale Services
Sunnyda is your ultimate destination for all your cold storage needs. Our comprehensive approach covers everything from designing and producing to installing and providing after-sales support for your cold rooms.
We pride ourselves on offering super-high efficiency products, backed by stringent quality control measures and a dedicated after-sales service system to ensure seamless operation. We also provide detailed user manuals for your convenience.
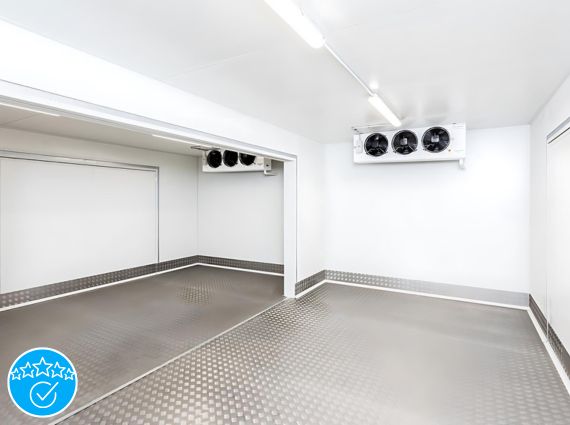

Discover Sunnyda's Large Cold Room Solution







Help to Find Your Large Cold Room Related Products



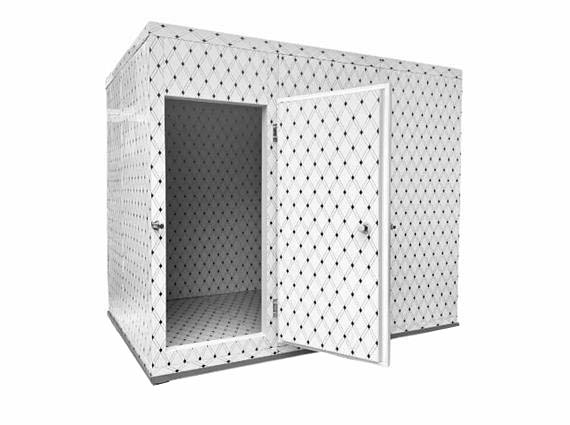
What is a Large Cold Room?
A large cold room is a highly specialized and meticulously engineered space designed to maintain consistently low temperatures. It is equipped with state-of-the-art refrigeration systems and advanced insulation to create an environment that ensures precise temperature control. With its expansive size and impressive capacity, the cold room can accommodate and preserve large quantities of perishable goods, making it an invaluable asset for businesses operating in industries such as food and beverage, pharmaceuticals, and chemicals. The cold room’s primary function is to preserve the quality of products, prevent spoilage, and support efficient supply chain operations, playing a crucial role in maintaining the integrity and safety of the goods stored within it.

Benefits of a Large Cold Room
Increased Storage Capacity
Accommodates larger volumes of products, reducing the need for frequent restocking. This feature allows you to manage inventory more efficiently and can help save time and effort by minimizing the frequency of restocking.
Product Preservation
Ensures that the product maintains its high quality and freshness for an extended time, preserving its flavor, texture, and nutritional value.
Improved Product Quality
Maintaining consistent temperature and humidity levels is essential for preserving the freshness and quality of products. By carefully controlling these factors, Sunnyda can ensure that items remain in optimal condition for extended periods, reducing waste and ensuring your satisfaction.
Energy Efficiency
Consolidating multiple smaller refrigeration units into a single, larger unit can lead to improved energy efficiency. This is because a larger unit generally has better insulation and more advanced technology, which can reduce the energy consumption required to maintain low temperatures.
Reduce Food Waste
To prevent product spoilage and extend shelf life, it is crucial to maintain precise temperature control and minimize product damage by implementing rigorous tracking and organization. This helps reduce the risk of expired goods, minimizes shrinkage, and improves operational efficiency. Large cold storage facilities are essential for fighting food waste and promoting environmental sustainability and economic efficiency.

Application of Large Cold Room
Food and Beverage Industry
Large cold rooms play a crucial role in the food and beverage industry. They are essential for preserving fresh produce, processing meat and seafood, storing dairy products, and maintaining frozen foods. These facilities facilitate efficient distribution and product development, ensuring product safety, extending shelf life, and reducing waste. As consumer demands for fresh and high-quality products continue to grow, large cold rooms have become indispensable in meeting these demands.
Pharmaceutical Industry
The pharmaceutical industry heavily relies on large cold rooms to ensure the integrity and potency of vaccines, maintain drug stability, store biological samples, and support clinical trials. These facilities play a crucial role in preserving the efficacy of pharmaceutical products while also upholding patient safety and meeting regulatory standards. Given this, the pharmaceutical industry has come to acknowledge the critical significance of large cold storage rooms in maintaining the proper storage and preservation conditions for temperature-sensitive pharmaceutical products. These spacious and meticulously controlled environments are essential for upholding the quality and effectiveness of such products, thereby contributing significantly to the overall success of the pharmaceutical industry.
Chemical Industry
Large cold rooms play a crucial role in the chemical industry by providing precisely controlled environments that are essential for maintaining the integrity and stability of temperature-sensitive chemicals. These specialized facilities enable meticulous storage, ensuring safe handling and transportation, supporting essential research and development processes, and ensuring compliance with safety and regulatory standards. As a result, these cold rooms are vital for the overall success of chemical operations.
Floral Business
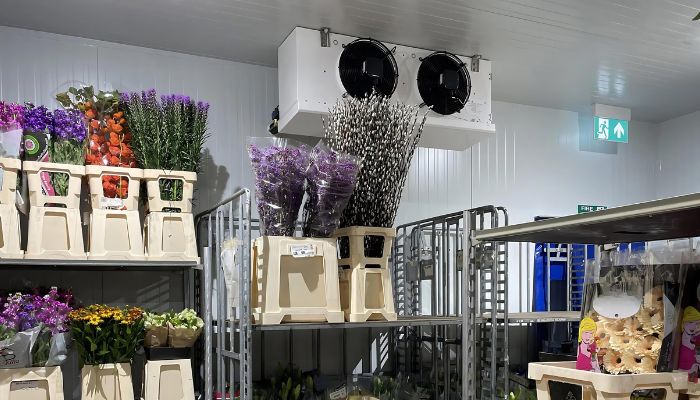
The floral industry is highly dependent on precise temperature control to safeguard the fragile properties of flowers, prolong their shelf life, reduce wastage, and uphold uniform quality. Cold storage is crucial in preserving product freshness, meeting customer expectations, and optimizing inventory management in the floral sector.